Welding looks simple from a distance: bright arc, steady hand, metal joined together. Up close, it is a controlled process built around safety, clean material, good fit-up, machine settings, shielding, heat control, and honest inspection. A beginner does not need to know everything on day one, but the first setup should be careful enough that each practice bead teaches something useful.
The goal at the start is not to repair a trailer, build a railing, or weld anything that could hurt someone if it fails. The goal is to learn how metal behaves, how the puddle moves, how sparks travel, how smoke is handled, and how a weld can look decent while still being weak. Treat the first sessions as shop practice, not as proof that every metal problem is now a welding project.
A: Controlled practice samples and useful observations, not a trailer repair or another safety-critical component.
A: No. Confirm whether the exact consumable is self-shielded or requires an external shielding gas.
A: Not necessarily. Assess the actual exposure and provide controls appropriate to the process, material, and workspace.
A: Do not weld used containers as a beginner project; residual contents and vapors can create severe explosion hazards.
A: No. Identify the product and hazards first, and use an approved preparation procedure with residues removed as required.
A: No. Surface smoothing cannot create fusion that the welding operation failed to produce.
A: No. Sound may help describe operation, but joint quality needs inspection appropriate to its intended use.
A: No. Check setup and preparation, then make a controlled adjustment whose effect you can compare.
A: After safe setup and repeatable movement are becoming familiar, use comparable coupons and qualified feedback.
A: Structural, pressure-containing, lifting, road-going, and other safety-critical fabrication requires appropriate design, procedures, skill, and verification.
Start With Safety, Not the Machine
The welder is only one part of the setup. Before an arc is struck, the area needs to be safe for heat, sparks, smoke, and bright light. Welding throws hot particles farther than beginners expect, and grinding can do the same. Cardboard, sawdust, rags, paint cans, plastic bins, gasoline, aerosol cans, and open dust collection should not be near the work.
Keep an appropriate fire extinguisher close, know how to use it, and stay in the area after welding long enough to catch smoldering material. Sparks can disappear behind a bench, under a cabinet, or inside a pile of debris. A clean concrete or steel work area makes learning easier because the student is not also managing hidden fire hazards.
Protect Your Eyes and Skin
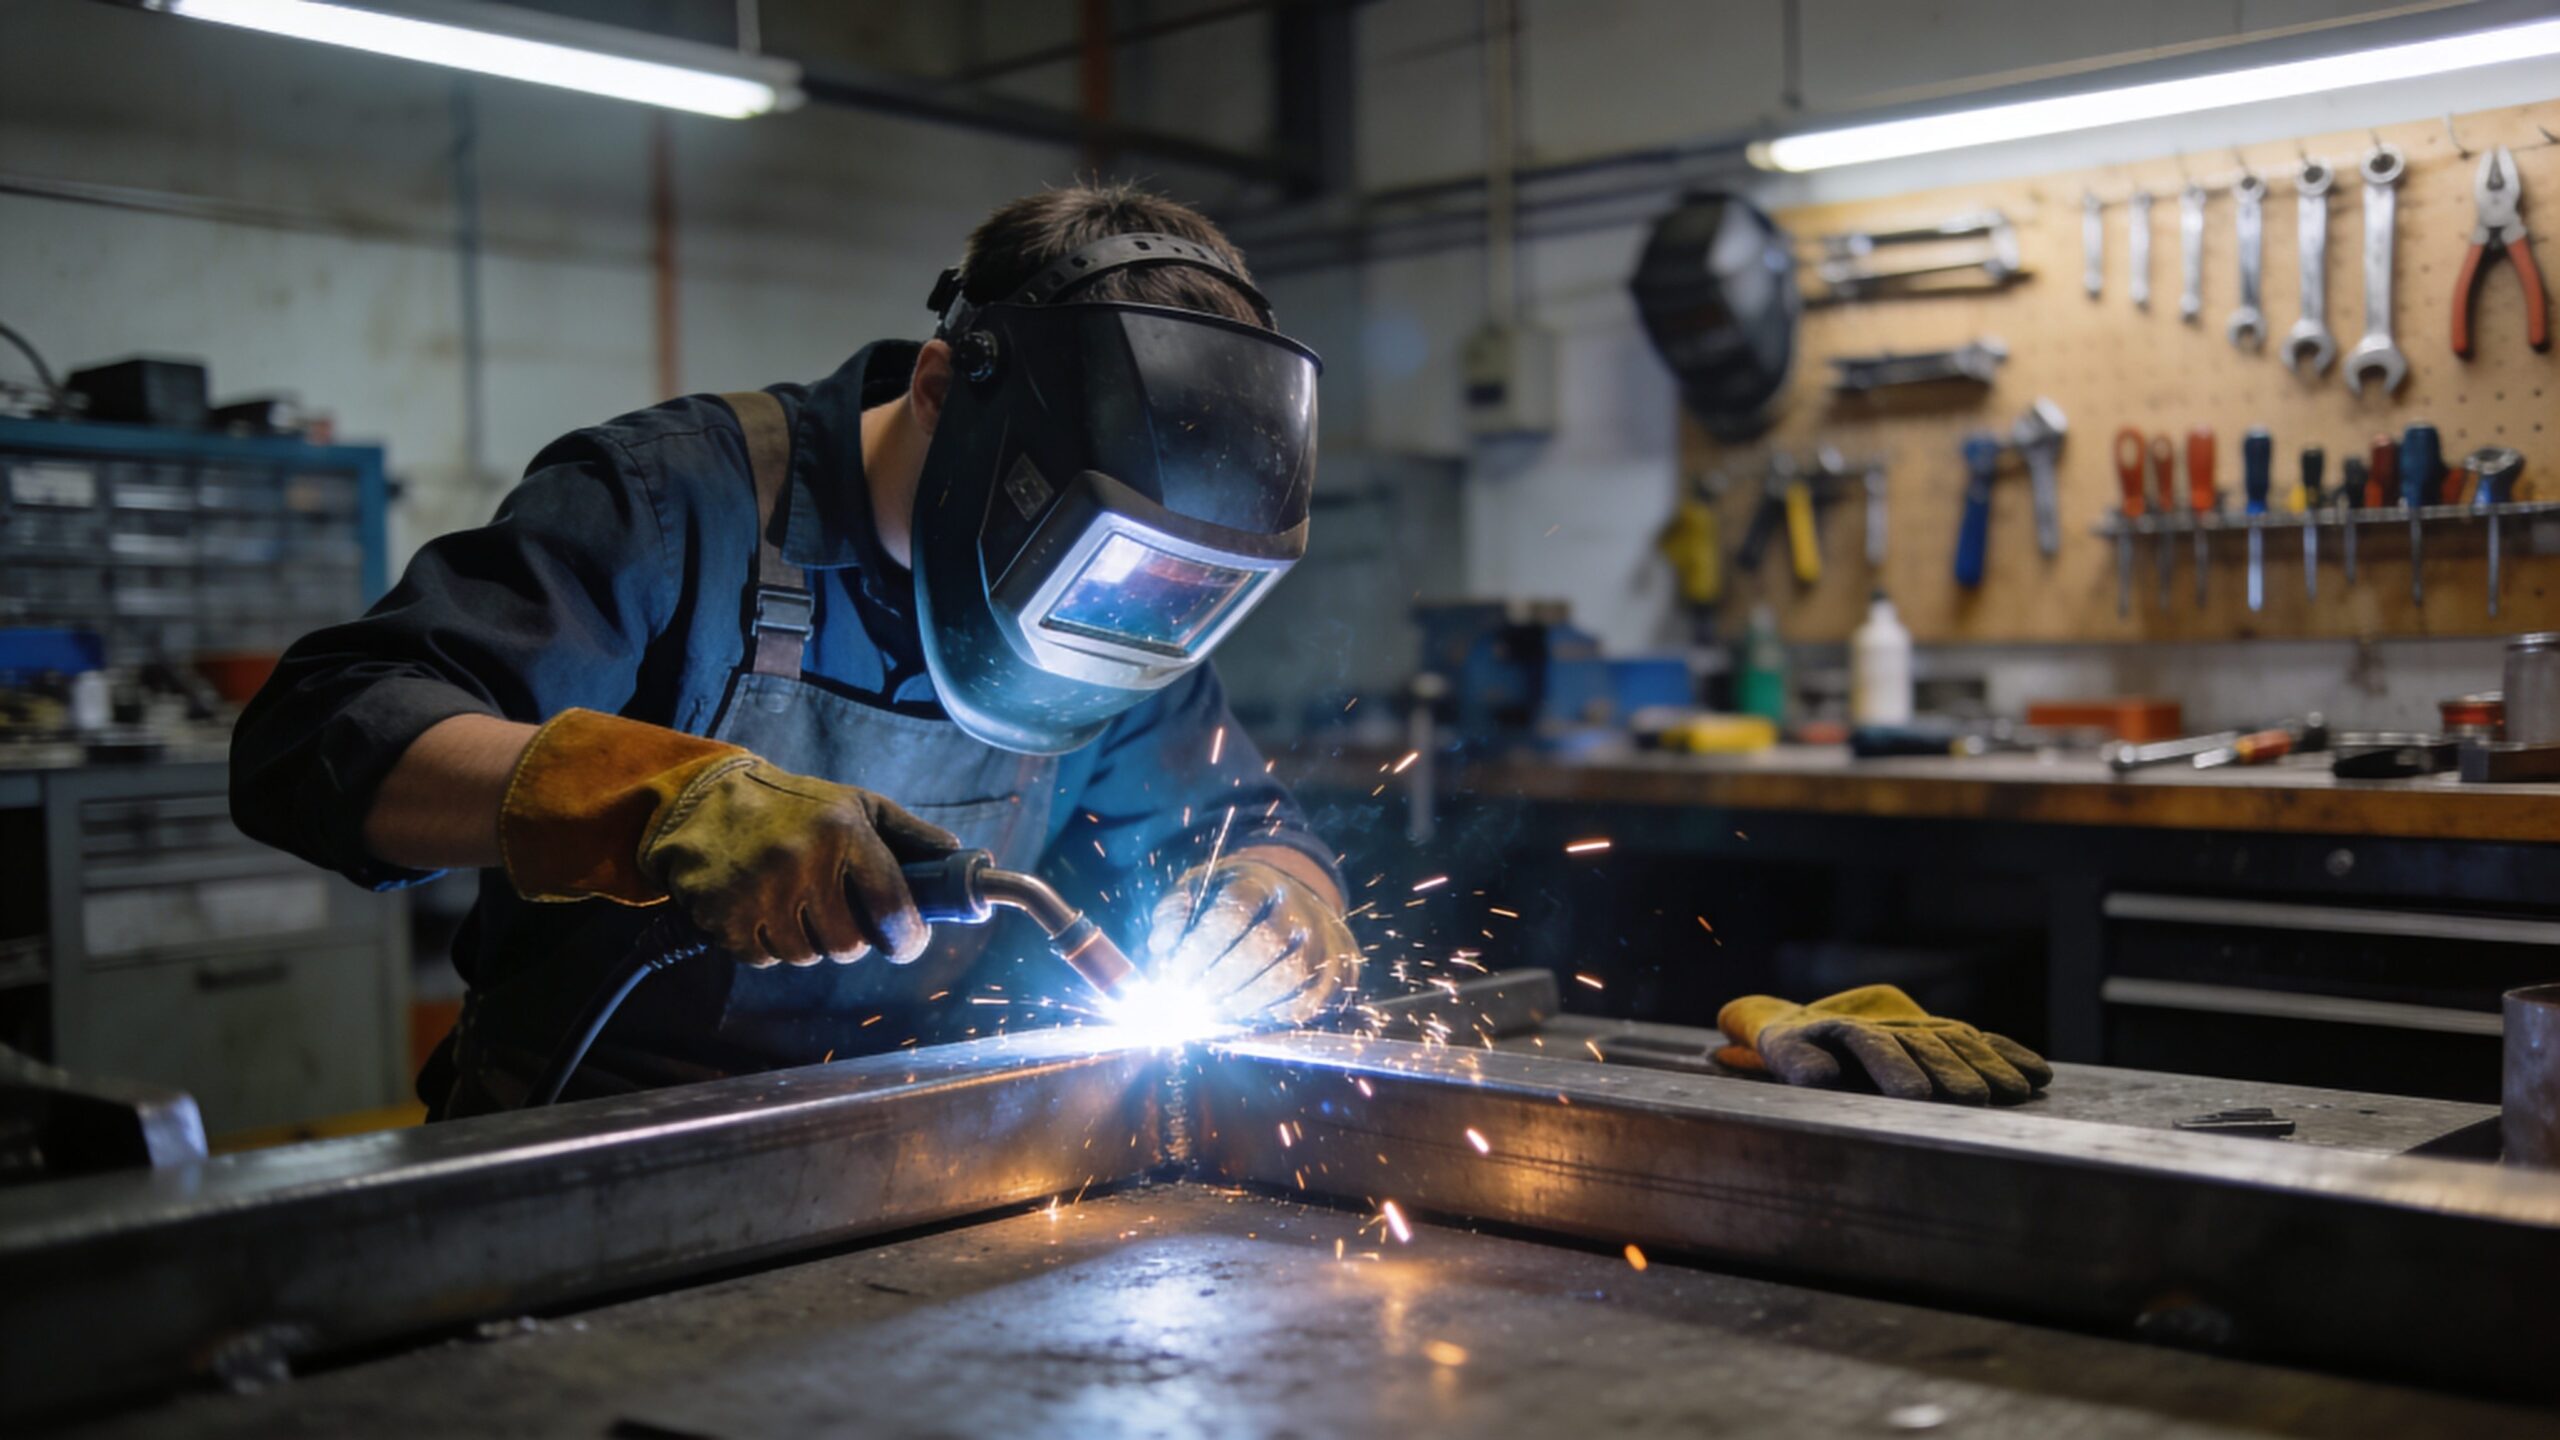
A proper welding helmet protects against arc flash and lets you see the puddle. Auto-darkening helmets are convenient, but they still need the right shade setting, clean lenses, good batteries if required, and a fit that blocks stray light. Safety glasses should be worn under the helmet because chipping, wire brushing, and grinding can send debris around the helmet.
Skin protection matters too. The arc can burn exposed skin like intense sunlight, and hot spatter can land in cuffs, pockets, shoes, or gloves. Wear welding gloves, natural-fiber clothing or a welding jacket, closed leather shoes or boots, and hearing protection when grinding or working around loud shop tools. Synthetic clothing can melt, which makes it a poor choice around sparks.
Think About Ventilation
Welding fumes are not just unpleasant; they can be harmful. The risk changes with the metal, coating, filler, process, and workspace. Clean mild steel is one thing. Galvanized metal, painted metal, stainless steel, unknown scrap, oily parts, or plated hardware can produce fumes that should not be inhaled.
Work in a ventilated area without letting a strong breeze ruin shielding gas. Do not weld on galvanized or coated metal unless you understand the hazard and have the right controls. For many beginners, the best first practice material is clean mild steel bought for practice, not random metal pulled from a pile.
Choose a Beginner-Friendly Process
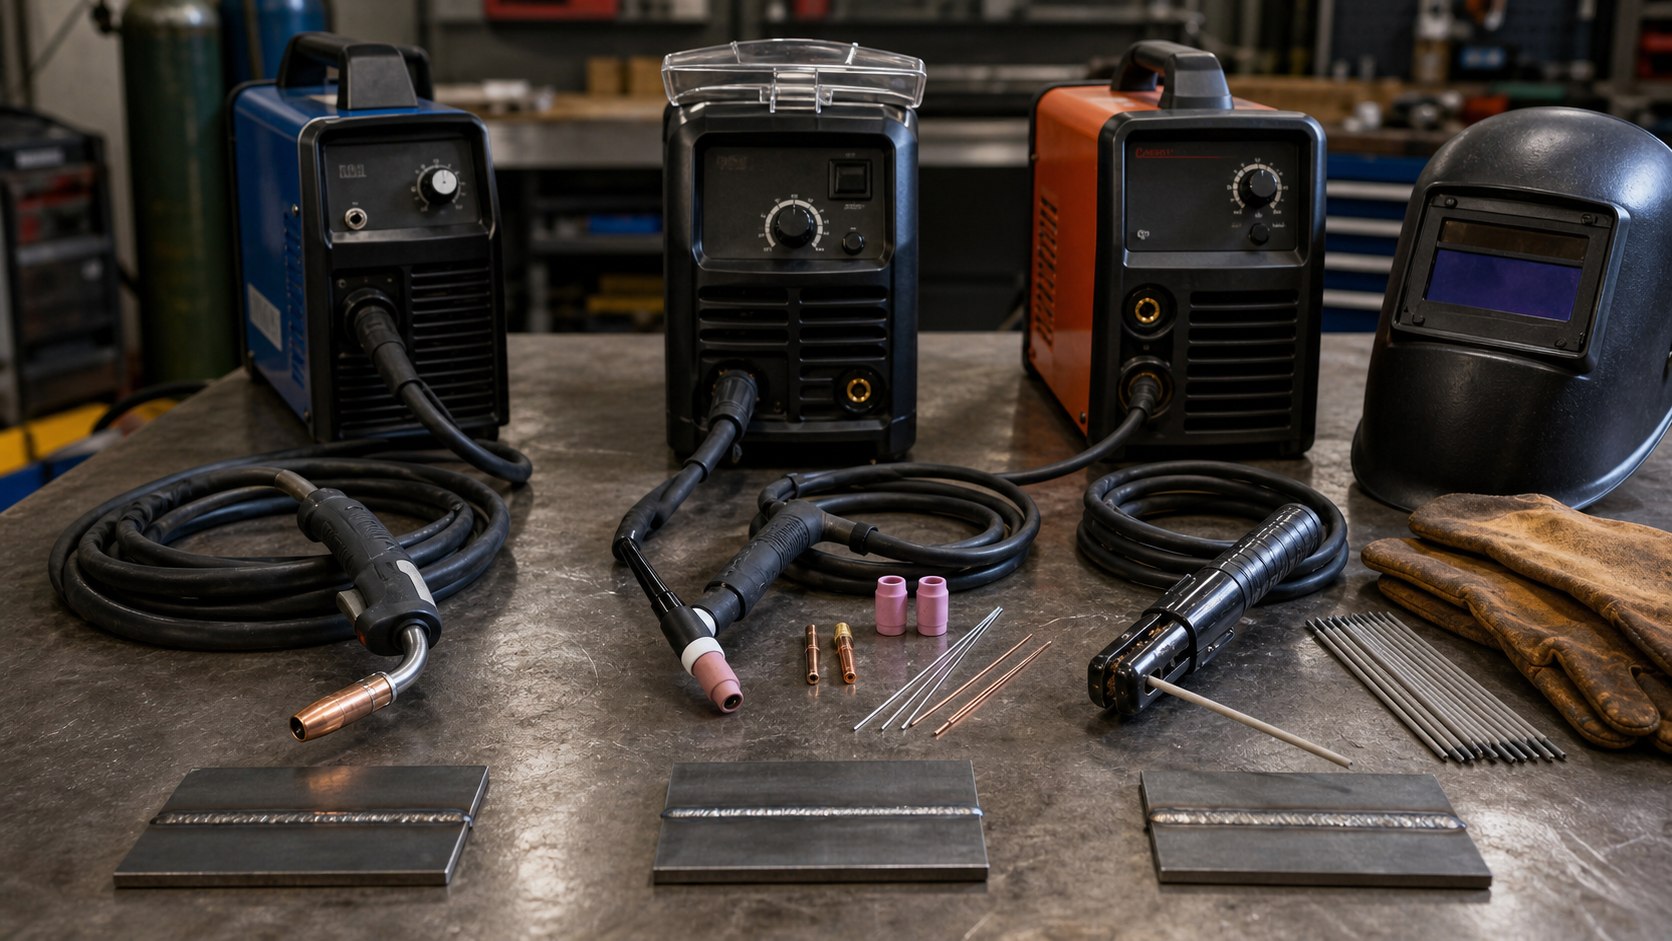
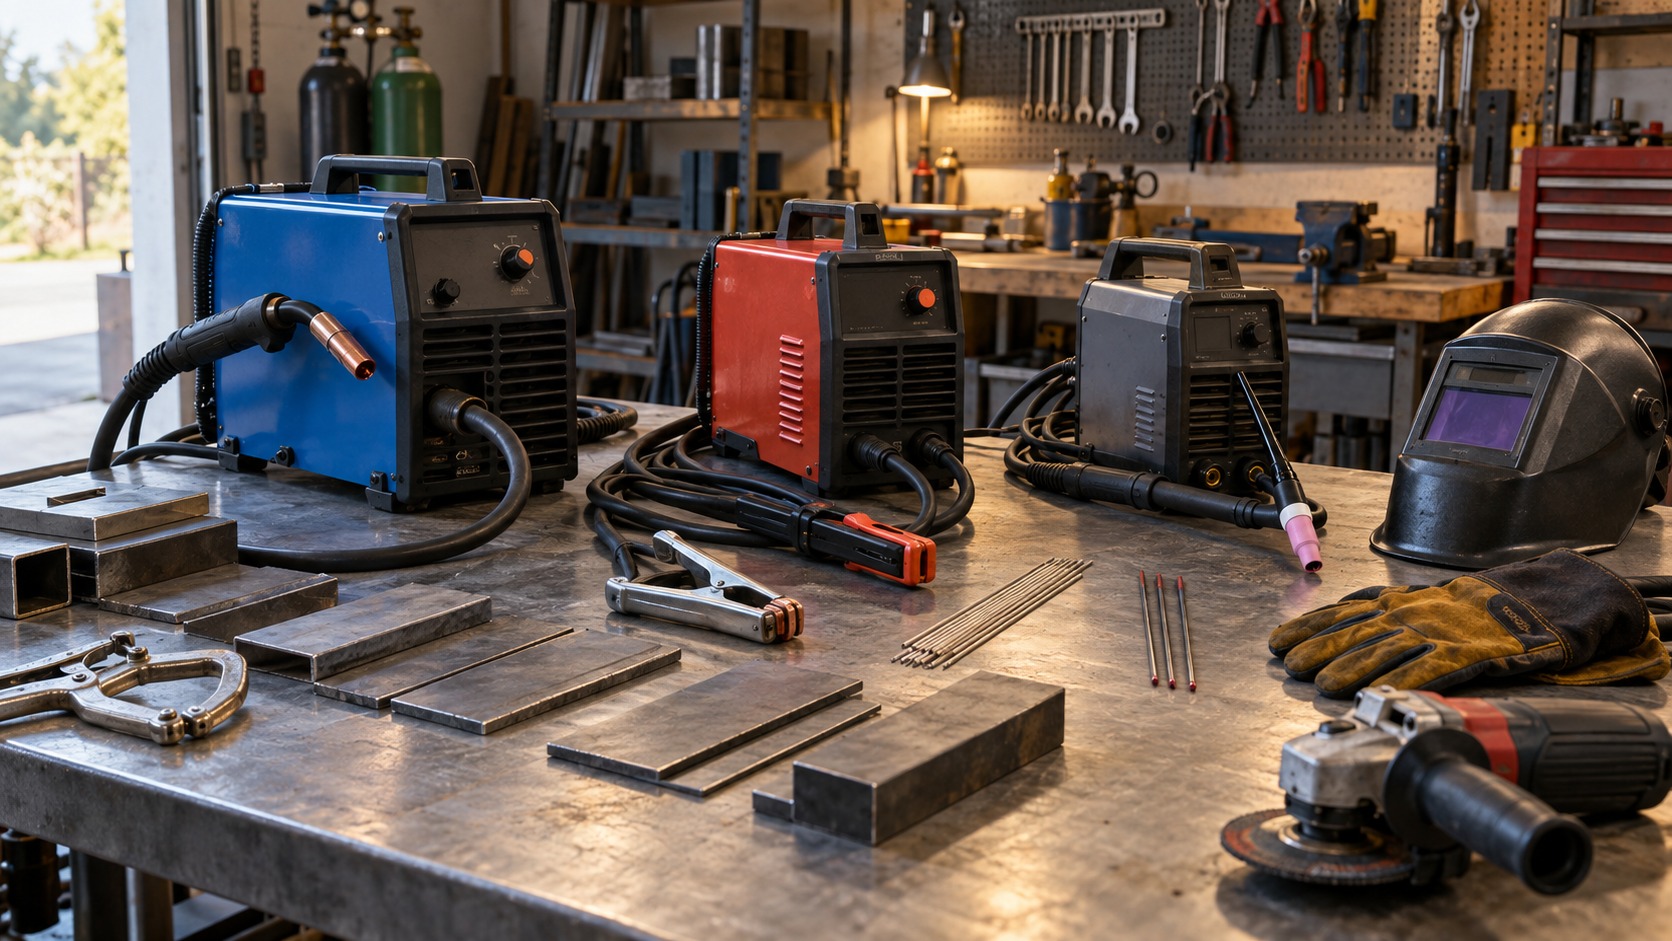
MIG, flux-core, stick, and TIG all join metal, but they do not feel the same for a beginner. MIG with shielding gas is often the easiest to learn on clean mild steel because the wire feeds continuously and slag cleanup is minimal. Flux-core can be useful outdoors because it does not rely on bottled gas in the same way, but it produces more smoke and slag.
Stick welding is rugged and versatile, especially outdoors and on thicker steel, yet arc starts, rod angle, slag, and sticking electrodes can frustrate a new welder. TIG offers excellent control and clean results, but it asks for coordination with torch, filler, foot pedal or amperage control, and tight fit-up. The best first process is the one that matches the material, workspace, and patience available.
Know What Your Welder Can Actually Do
A small 120-volt welder can be great for practice, thin steel, small brackets, carts, and light fabrication. It is not magic. Every machine has limits for material thickness, duty cycle, wire size, electrode size, amperage range, and power supply. Pushing a small machine beyond its comfort zone creates frustration and weak welds.
Read the chart inside the machine door or the manual before guessing. The chart is not perfect, but it gives a starting point for wire speed, voltage, amperage, polarity, and material thickness. Make changes one at a time so you know what helped.
Use Clean, Known Practice Metal
Practice goes better on metal that is clean and predictable. Mild steel coupons, flat bar, angle iron, and square tube are good learning materials because they let you repeat the same joint several times. Avoid rusty, painted, oily, galvanized, or mystery metal for early practice because each contaminant changes the arc and the finished weld.
Clean mill scale, rust, paint, oil, and cutting residue from the weld zone with a grinder, flap disc, wire brush, or solvent used safely before welding. The weld only happens where molten metal can tie into clean base metal. If the surface is dirty, the bead may sit on top, pop, smoke, or develop porosity.
Understand Fit-Up Before You Strike an Arc
Fit-up is how well the parts meet before welding. Gaps, uneven edges, poor contact, and loose parts make welding harder. A beginner often blames the machine when the real problem is that the joint is moving or the edges do not line up.
Use clamps, magnets, squares, and a stable table to hold parts in position. Tack weld first, then recheck alignment. Welding shrinks metal as it cools, so parts can pull out of square. Short tacks placed thoughtfully are easier to correct than a full weld that dragged the project out of shape.
Ground the Work Correctly
The work clamp needs clean metal and a solid connection. A poor ground can cause erratic arc starts, spatter, weak heat, and confusing symptoms. Clamp to the workpiece or to a clean metal table that has good contact with the work.
Do not clamp over paint, heavy rust, loose scale, or a tiny edge that barely holds. If the arc sounds inconsistent and the machine settings seem reasonable, check the ground before chasing every other possibility.
Learn the Puddle, Not Just the Bead
The visible bead is the result. The puddle is the live molten area that tells you what is happening while welding. Beginners often stare at the sparks or nozzle. Try to watch the leading edge of the puddle and the way it wets into both sides of the joint.
A good practice session includes stopping often and asking what you saw. Did the puddle wash into both pieces? Did it pile up cold on one side? Did the arc dig a groove at the edge? Did the travel speed leave a tall rope or a thin overheated line? Seeing the puddle is a skill that grows with repetition.
Practice Flat Beads First
Before building anything, run straight beads on flat plate. This removes joint fit-up from the lesson and lets you focus on distance, angle, speed, and settings. Run several beads side by side, then compare them after brushing or chipping.
Look for consistency. The bead should be reasonably even, not randomly narrow and wide. Spatter, undercut, porosity, and cold edges are clues. The first goal is not beauty; it is learning what changes when the hand moves faster, slower, closer, farther, steeper, or flatter.
Move Into Basic Joints
Once flat beads make sense, practice joints. Butt joints, lap joints, T-joints, and outside corners each teach something different. A lap joint can hide lack of fusion if you only look at the top. A T-joint requires tying into two surfaces. A butt joint shows whether the edges were prepared and aligned.
Use the same material thickness for repeated practice. If every coupon is different, it becomes harder to learn from the results. Keep a few pieces unground so you can compare bead shape and remember what each setting produced.
Inspect Before Grinding
Grinding can make a weld look cleaner while hiding the information you need. Before smoothing anything, look at the bead edges, start and stop points, width, height, toe lines, discoloration, slag, porosity, and distortion. If the weld failed to tie in, grinding the crown will not make it stronger.
For practice pieces, cut, bend, hammer, or break samples when safe and reasonable. Destructive testing teaches more than staring at a pretty bead. A weld can look acceptable on top and still lack penetration or fusion inside the joint.
Understand Common Weld Problems
Porosity looks like holes or pinpricks and can come from contamination, poor gas coverage, wind, damp consumables, or dirty metal. Undercut is a groove melted along the edge of the weld that was not filled back in. Cold lap happens when weld metal rolls onto the base metal without fusing properly. Burn-through occurs when thin metal overheats and opens up.
Spatter, slag inclusion, excessive buildup, cracking, and warping are also clues. Do not treat defects as random bad luck. They point back to a cause: settings, travel speed, angle, prep, shielding, fit-up, or heat input. One defect at a time is easier to solve than changing everything at once.
Change One Variable at a Time
Beginners improve faster when practice is controlled. If a weld looks poor and you change voltage, wire speed, angle, travel speed, and metal prep all at once, you will not know what helped. Make one adjustment, run another bead, and compare.
Keep quick notes. Record material thickness, process, wire or rod size, gas if used, machine settings, joint type, and what the bead looked like. A phone photo of the settings and coupon can be enough. Notes turn practice from guessing into learning.
Control Heat and Distortion
Welding pulls metal as it heats and cools. Long welds, thin material, poor tack placement, and too much heat can bend a project out of shape. Beginners often discover this after a frame, bracket, or panel no longer sits flat.
Use tacks, skip around, let parts cool, clamp where appropriate, and avoid overwelding. More weld is not always better. The right weld in the right place is stronger and cleaner than a giant bead that overheats the part.
Respect Thin Metal
Thin metal is harder than it looks. It burns through quickly, warps easily, and punishes slow travel or high heat. Automotive sheet metal, thin tube, appliance panels, and decorative pieces require more control than many first-time welders expect.
Practice on scrap of the same thickness before touching the real part. Short tacks, cooling time, copper backing, lower settings, and careful fit-up can help, but thin metal is not the best place to learn the basics from scratch.
Know When Stick Welding Makes Sense
Stick welding can handle outdoor work, dirty conditions, thicker steel, and repairs where portability matters. It also teaches arc length, puddle control, and slag management. The tradeoff is that starts, restarts, rod angle, and slag cleanup add difficulty.
If stick welding is your first process, use clean practice steel and an electrode that matches the machine and material. Learn to restart cleanly and remove slag fully before judging the weld. Slag left in a joint can create weakness even when the bead looks full.
Understand Shielding Gas Basics
Gas-shielded MIG needs adequate gas flow and protection from wind. Too little flow can leave the weld porous. Too much flow can create turbulence that pulls air into the shielding area. A breeze from a fan, open garage door, or outdoor work area can defeat the gas coverage.
Check the gas cylinder, regulator, hose, fittings, and nozzle. Keep the nozzle clean enough that shielding reaches the puddle. If porosity appears suddenly on clean steel, gas coverage is one of the first things to inspect.
Use Consumables That Match the Job
Wire, rods, contact tips, nozzles, cups, tungsten, and shielding gas are not interchangeable details. They affect arc stability, penetration, cleanup, and bead appearance. A machine set up for one wire size may not feed another size well without changing tips or drive settings.
Store consumables properly. Damp electrodes, rusty wire, dirty tips, and clogged nozzles make learning harder. When a beginner is fighting bad consumables, every lesson becomes blurry.
Do Not Start With Safety-Critical Repairs
Some projects should wait until skill, testing, and professional judgment are much stronger. Vehicle frames, trailer hitches, lifting points, ladders, pressure vessels, roll cages, structural supports, gas containers, and load-bearing repairs are not beginner practice pieces.
There is no shame in starting with coupons, shop hooks, small carts, tabs, stands, or noncritical brackets. Those projects still teach layout, fit-up, tacking, heat control, and finishing without putting people at risk if a weld fails.
Choose a Useful First Project
After scrap practice, pick a small project that is useful but forgiving. A welding cart accessory, grinder stand, small shelf bracket, practice frame, or simple shop hook can be a good step. The project should use material thick enough to weld comfortably and joints simple enough to inspect.
Keep the first project square, modest, and measurable. If the part twists, the bead is inconsistent, or the tacks pull out of position, the lesson is still valuable. The best first project gives feedback without pretending to be a professional fabrication job.
Prepare for Grinding and Finishing
Welding usually brings grinding, wire brushing, cutting, drilling, and surface prep. These steps need their own safety habits. Sparks from a grinder can travel farther than welding sparks, and cutoff wheels deserve respect. Use guards, eye protection, hearing protection, and the right disc for the task.
Do not grind every weld flat just because it is visible. On some projects, grinding can weaken a weld or remove useful evidence. On decorative work, finishing matters, but the weld should still be inspected before it disappears under a flap disc and paint.
Think About Paint and Corrosion
Freshly welded steel can rust quickly, especially after grinding. If the project will live outdoors or in a damp shop, plan for cleaning, primer, paint, or another protective finish. Welds, cut edges, and ground areas need coverage just as much as the flat faces.
Remove slag, soot, oil, and dust before finishing. Paint over contamination fails early. A simple shop project looks better and lasts longer when the finishing step is treated as part of the build rather than cleanup after the interesting work is over.
Build a Practice Routine
A good beginner routine is simple: set up the area, clean the metal, check PPE, clamp the work, verify settings, run short welds, inspect, take notes, and change one variable. Repeat that cycle on scrap before building. The repetition creates muscle memory and judgment.
Stop before fatigue turns into sloppy work. Welding while tired leads to careless handling of hot parts, missed fire hazards, and bad decisions. Short, focused sessions often teach more than a long session where every bead gets worse.
Learn the Sound, But Verify the Result
Experienced welders often talk about sound because arc stability can be heard. A steady MIG arc may sound smooth and consistent, while a poor setup can pop, hiss, or surge. Sound is helpful, but it is not inspection.
Always look at the result. Brush or chip the bead, inspect the edges, check the back side when possible, and compare the weld to the settings and prep. A weld that sounded fine can still have defects if the joint was dirty, poorly fitted, or shielded badly.
Know When to Ask for Help
Welding has real consequences, and good welders keep learning. Ask an experienced welder, instructor, or qualified professional to look at practice pieces when possible. A second set of eyes can point out undercut, cold lap, poor tie-in, or heat problems that a beginner may miss.
Professional help is especially important for anything structural, pressurized, road-going, overhead, or safety-related. Learning to weld is valuable, but knowing when a job is beyond your current ability is part of becoming safer and better.
Keep the First Goal Realistic
The first goal is not a perfect bead. It is a safe setup, clean material, steady practice, and honest inspection. If you can repeat a bead, explain what changed, recognize obvious defects, and keep the work area safe, the session is successful.
Welding rewards patience because each small improvement builds on the last. Clean one joint better. Hold the gun steadier. Adjust one setting. Watch the puddle longer. Let the metal cool. Over time, those habits matter more than any single dramatic spark-filled moment.